What Are You Looking For?
Latest News & Blog
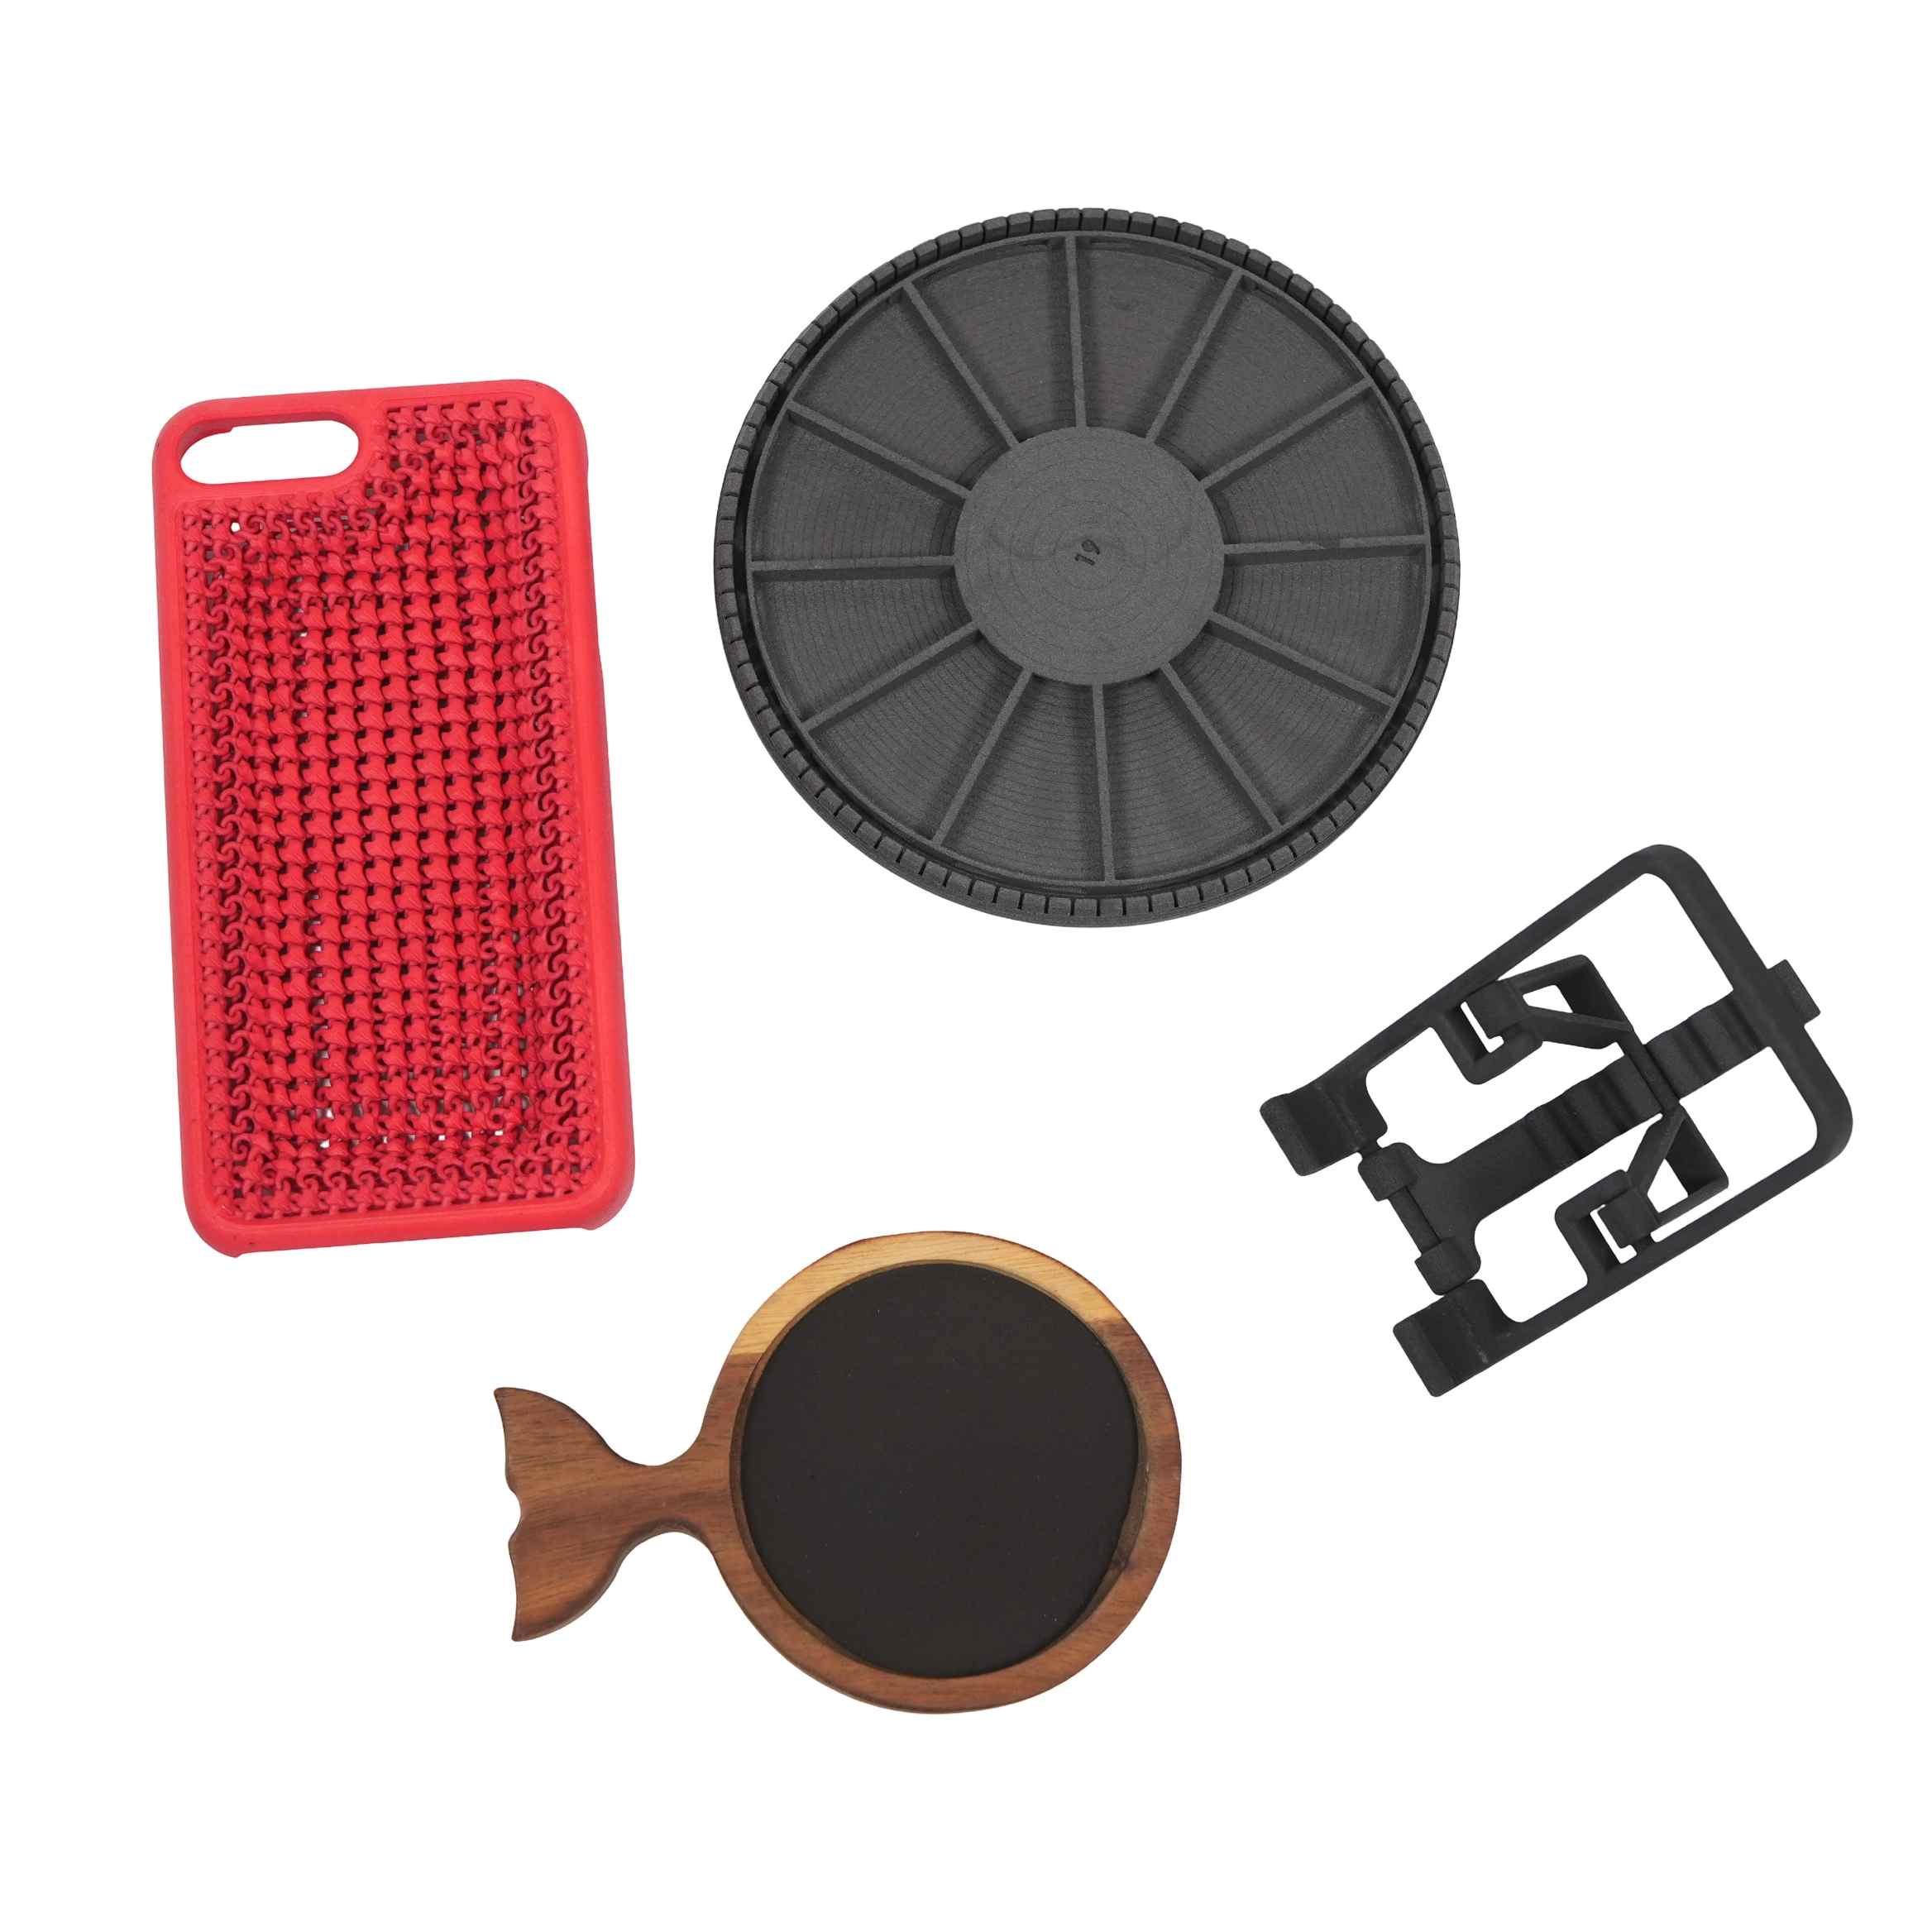
Industrial Selective Laser Sintering (SLS) technology is undergoing a decisive evolution, shifting rapidly from fast aesthetic prototyping to direct digital manufacturing of functional end-use components. As industrial enterprises integrate additive systems into series production, the demand for repeatable part accuracy, zero internal defects, and consistent isotropic mechanical properties has never been higher. Achieving these strict production standards requires a deep understanding of polymer behavior during laser scanning and thermal cooling. Partnering with a reliable Advanced PA12 Powder For SLS Printing Manufacturer allows engineering teams to identify the root causes of common printing defects, adjust material parameters, and optimize powder bed interactions effectively. Industry Shift: Transitioning SLS from Rapid Prototyping to Low-Volume Direct Production The transition toward Direct Digital Manufacturing fundamentally transforms how engineering teams evaluate SLS raw materials. While aesthetic prototypes tolerate minor surface roughness or slight internal voiding, functional end-use components require uncompromising mechanical integrity and tight dimensional tolerances. Consequently, manufacturing engineers must ensure that every printed layer consolidates uniformly across the entire build platform. Material performance serves as the cornerstone of this manufacturing transition. Variations in powder particle morphology, thermal stability, or viscosity can lead to unpredictable mechanical failures under operational stress. With over 17 years of specialized expertise in polymer modification, Xiamen Bocheng Plastic Materials Co., Ltd provides technical insights that connect polymer powder chemistry directly to real-world printing performance. Understanding these underlying material dynamics helps operators solve persistent quality challenges and achieve reproducible production yields. Diagnostic Guide 1: Eliminating Surface "Orange Peel" Through Particle Size Distribution Control Surface roughing, commonly known as the "orange peel" effect, remains one of the most frequent defects in SLS components. This issue typically stems from uneven powder bed spreading, erratic fluidization, and localized melt agglomeration during laser scanning. When powder contains an excessive concentration of fine particles or an overly broad particle size distribution, recoater blades create drag marks across the build area. Different polymer processing methods require specific particle size profiles to function efficiently. For example, electrostatic spraying techniques typically utilize particles with a median diameter (D50) between 35 and 45 micrometers to optimize surface charge adhesion. Conversely, fluidized bed dip coating relies on coarser particles ranging from 80 to 120 micrometers for gravity immersion. For industrial SLS additive manufacturing, optimal performance requires a strictly controlled spherical distribution where D50 ranges from 45 to 50 micrometers, D10 remains between 25 and 30 micrometers, and D90 stays within 70 to 75 micrometers. Maintaining a tight particle size distribution span—calculated as Span = (D90 - D10) / D50—below 1.0 prevents powder segregation. To address this technical hurdle across specialized 3D printing applications, BOCHENG employs sub-zero cryogenic milling at minus 100 degrees Celsius followed by precision multi-stage air classification. This process yields the BC-PA12-S01 grade, which features a uniform bulk density between 0.45 and 0.50 grams per cubic centimeter and a low angle of repose at 32 degrees. These physical properties ensure smooth fluidization, consistent layer deposition, and smooth surface finishes free of orange peel defects. Diagnostic Guide 2: Solving Internal Porosity via Optimized Powder Refresh & Viscosity Management Internal porosity severely compromises the tensile strength, impact resistance, and fluid tightness of printed parts. Microscopic voids inside the component usually develop when the molten polymer exhibits high melt viscosity, which prevents complete particle coalescence before solidification occurs. This elevated viscosity frequently results from thermal aging when virgin powder mixes with recycled material that has undergone multiple heating cycles. During extended printing runs, polyamide powders experience post-condensation reactions in the build chamber. This thermal exposure increases molecular weight and lowers the Melt Flow Rate (MFR). Consequently, heavily aged powders fail to flow together smoothly when struck by the laser beam, trapping air pockets between powder granules. Managing the refresh ratio—the proportion of virgin powder added to used powder—is crucial for maintaining consistent rheological properties. To eliminate internal voiding, BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd) formulates its PA12 materials with proprietary heat-stabilizing additives that broaden the sintering window to 20–30 degrees Celsius. Featuring a precise melting point of 181 degrees Celsius and a crystallization temperature between 145 and 155 degrees Celsius, the material resists thermal degradation during prolonged build cycles. As a result, operators can maintain a flexible refresh ratio between 30% and 70% while keeping internal part porosity under 1%, preserving both structural integrity and operational cost efficiency. Diagnostic Guide 3: Overcoming Poor Interlayer Adhesion & Warpage via Thermal History Control Interlayer delamination and part curling present significant obstacles to achieving dimensional accuracy and isotropic strength. These defects occur primarily when build chamber temperature gradients fluctuate outside the strict sintering window. If the bed temperature drops below the crystallization threshold—typically kept between 165 and 175 degrees Celsius—the polymer crystallizes prematurely, creating internal contraction stress and layer warping. Controlling the thermal history of the powder bed throughout multi-hour print runs prevents uneven crystallization shrinkage. Furthermore, excess moisture in raw powders can cause hydrolytic degradation at elevated temperatures, leading to unpredictable mechanical properties and weak layer bonding. Maintaining rigorous control over environmental storage conditions and raw material specifications eliminates these variable parameters. Engineers address these challenges by enforcing strict raw material moisture thresholds below 0.1%. Comprehensive five-stage quality control testing across every production batch guarantees predictable thermal absorption during laser scanning. This uniform thermal response minimizes inter-layer boundary weakening and delivers consistent z-axis shear strength, ensuring that complex structural components remain flat and dimensionally stable. Beyond Standard PA12: Advanced SLS Portfolio & OEM Supply Capabilities As industrial applications diversify, specialized polymer formulations are required to meet demanding mechanical and thermal specifications. Beyond standard polyamide powders, specialized composite grades expand the functional capability of additive manufacturing equipment in automotive, aerospace, and consumer goods sectors. The composite portfolio includes BC-PA12-GF-S01, a glass-reinforced powder containing 20% to 25% glass spheres that achieves a Heat Deflection Temperature (HDT at 1.8 MPa) of 168 degrees Celsius for rigid structural enclosures. Additionally, BC-PA12-CF-S01 incorporates 25% to 30% carbon fibers to deliver a tensile modulus of 4500 MPa for lightweight functional parts. For applications demanding high impact resistance or flexibility, BC-PA11-S05 provides elongation at break exceeding 30%, while BC-TPU-S90 offers elastomeric performance rated at Shore 90A. To support global industrial supply chains, products are packaged in 25-kilogram heavy-duty moisture-proof sealed containers to ensure long shelf life during transit. Customized powder color options and material property modifications are also available to meet specific OEM manufacturing requirements. BOCHENG supports international clients with efficient delivery turnaround times of 7 to 15 days, supported by flexible global trade settlement channels including T/T and VTB Bank options. Operating under ISO 9001 and IATF 16949 quality management certifications, alongside USP Class VI biocompatibility compliance, the enterprise continues to advance polymer materials for global additive manufacturing applications. For more technical documentation and product details, visit the official website: https://www.pa6-pa66.com/.
Read More
Industrial engineering demands continuous evaluation of lightweight composite materials. As global manufacturing scales up efficiency targets, high-performance Fiber Reinforced Nylon compounds play a crucial role in metal replacement projects. Polymer specifiers face a structural choice between carbon fiber (CF) and glass fiber (GF) reinforcements. While glass fiber has long dominated the market due to its low cost, carbon fiber is rapidly gaining ground in specialized structural applications. This comparative study analyzes the physical, electrical, and economic trade-offs between both filler technologies. Rather than declaring one material universally superior, objective evaluation shows that operational environment dictates the ideal choice. The Evolving Cost Curve: Will Carbon Fiber Redefine Industrial Nylon Selection? For decades, glass fiber reinforced polyamides served as the default choice for structural plastic components. The low production cost of E-glass fiber allowed compounding mills to produce high-strength materials at competitive price points. In contrast, carbon fiber precursors required energy-intensive carbonization processes, restricting carbon fiber composites to aerospace and high-end automotive sectors. However, recent advancements in precursor chemistry and large-tow fiber manufacturing have begun shifting this cost dynamic. The market price of commercial-grade carbon fiber continues a gradual downward trend. Consequently, design engineers now evaluate carbon fiber compounds for mainstream industrial applications where extreme weight savings justify a moderate price premium. Despite these cost improvements, glass fiber maintains a substantial price advantage. Raw glass fiber remains significantly cheaper per kilogram than carbon fiber. Therefore, complete market substitution will not occur. Instead, industrial manufacturers adopt a dual-track strategy. They utilize glass fiber for cost-sensitive structural housings and reserve carbon fiber for high-dynamic components that require exceptional stiffness-to-weight ratios. Functional Physics: Carbon Fiber vs. Glass Fiber Reinforcement Mechanics Understanding the physical mechanics of carbon fiber and glass fiber reveals distinct performance vectors across mechanical, electrical, tribological, and aesthetic dimensions. Strength-to-Weight Ratio and Lightweighting Carbon fibers possess a density of approximately 1.8 g/cm³, whereas glass fibers average around 2.5 g/cm³. Consequently, carbon fiber reinforced nylon compounds achieve higher specific strength and modulus at lower overall component weight. A 30% carbon fiber compound offers nearly double the flexural modulus of an equivalent glass fiber compound while reducing total mass by roughly 10%. Electrical Conductivity and EMI Shielding Glass fiber acts as an electrical insulator, making it suitable for high-voltage housings requiring dielectric strength. Conversely, carbon fiber exhibits intrinsic electrical conductivity. At filler loadings above 20%, carbon fiber creates a conductive percolation network within the nylon matrix. This network enables electrostatic dissipation (ESD) and electromagnetic interference (EMI) shielding without requiring secondary conductive additives. Tribology and Wear Resistance In moving mechanical assemblies, glass fibers act as abrasive particles that accelerate counter-surface wear over extended cycles. Carbon fibers, however, possess graphite-like crystalline structures that provide self-lubricating properties. Carbon fiber reinforced gears and bearings demonstrate lower friction coefficients and substantially lower wear rates than glass fiber alternatives. Surface Aesthetics and Finish Quality Glass fibers often cause surface defect issues, such as fiber read-through or floating fibers, on injection molded parts. Carbon fiber filaments disperse differently during melt processing, yielding a smooth, uniform matte black finish. This superior aesthetic appeal eliminates post-molding painting steps for exposed structural components. Matrix Chemistry & Filler Loadings: Deconstructing PA612 CF30/CF40 vs. Standard PA66 Formulations Composite performance depends heavily on the interaction between the fiber filler and the base polymer matrix. While standard PA66 resin offers high heat resistance and tensile strength, long-chain polyamides like Polyamide 612 (PA612) present unique advantages when paired with carbon fibers. PA612 possesses a lower density of amide groups compared to PA66, resulting in exceptionally low moisture absorption. Standard PA66 absorbs up to 2.5% moisture in ambient conditions, which alters part dimensions and reduces mechanical stiffness over time. In contrast, PA612 retains dimensional stability in humid environments and chemical contact. When examining filler loadings, CF30 (30% carbon fiber) and CF40 (40% carbon fiber) represent critical performance tiers. Increasing carbon fiber content from 30% to 40% in a PA612 matrix boosts tensile strength from roughly 210 MPa to over 240 MPa. Flexural modulus increases even more dramatically, reaching values above 22,000 MPa. However, higher filler loadings reduce impact toughness and increase melt viscosity. Compounders carefully adjust compounding parameters to balance structural rigidity with processing flowability. Application Boundary Mapping: Defining Optimal Operational Scenarios Clear operational boundaries determine whether carbon fiber or glass fiber delivers superior value for a given application. Aerospace brackets, commercial drone arms, robotic end-effectors, and medical equipment heavily favor carbon fiber reinforced polyamides. Drones require maximum flight time, where every gram of weight reduction directly extends battery life. Robotic arms require rapid acceleration with minimal inertia, making high specific stiffness essential. In contrast, high-volume industrial pump housings, power tool casings, and structural automotive brackets rely primarily on glass fiber reinforced polyamides. In these applications, thermal resistance and low unit costs outweigh maximum weight reduction. However, emerging hybrid demands in automotive and industrial parts manufacturing increasingly bridge these domains. Electric vehicle battery modules, for example, require EMI shielding and low structural mass, making carbon fiber polyamides a growing choice for next-generation vehicle architectures. Precision Compounding Expertise: The BOCHENG Technical Advantage Producing consistent carbon fiber and glass fiber compounds demands sophisticated manufacturing controls. Carbon fibers are brittle and break easily during melt extrusion, which severely reduces the aspect ratio and degrades final mechanical properties. The engineering team at BOCHENG(Xiamen Bocheng Plastic Materials Co., Ltd) uses specialized twin-screw extrusion systems with optimized shear profiles. This precision compounding technique prevents excessive fiber breakage while maintaining thorough fiber dispersion throughout the matrix. Furthermore, Xiamen Bocheng Plastic Materials Co., Ltd applies proprietary surface sizing agents that enhance interfacial bonding between carbon fibers and polyamide resins. Strong interfacial adhesion ensures efficient stress transfer from the polymer matrix to the reinforcing fibers. Operating under ISO 9001 and IATF 16949 quality standards, BOCHENG tests every production batch for tensile modulus, ash content, melt flow rate, and electrical resistivity. This rigorous quality framework guarantees that global customers receive material that meets exact engineering specifications. Strategic Conclusion: Aligning Performance Requirements with Material Reality Selecting between carbon fiber and glass fiber reinforced nylon requires an objective balance of mechanical targets, weight constraints, and production budgets. While glass fiber remains the most economical choice for general structural parts, carbon fiber offers irreplaceable functional benefits in conductivity, wear resistance, and high specific strength. By leveraging specialized formulations like PA612 CF30 and CF40, manufacturers achieve optimal performance tailored to harsh operational environments. Partnering with technical compounding specialists ensures long-term material consistency and engineering support. To review technical data sheets, request compound samples, or evaluate material selection for custom applications, visit https://www.pa6-pa66.com/.
Read More
Modern cordless power tools operate under increasingly demanding field environments. Industrial workers and heavy-duty contractors subject these tools to constant mechanical vibration, thermal elevation, direct impact, and harsh chemical exposure. Consequently, global original equipment manufacturers (OEMs) demand housing materials that offer an uncompromising balance of mechanical rigidity, drop-impact toughness, and strict flame retardancy such as UL94 V-0 standards. Engineering teams routinely turn to 30% glass fiber reinforced polyamide 6 compounds to fulfill these requirements. However, reliance on standard material data sheets frequently creates a false sense of security during project development. Insights from a leading China Top PA6 GF30 For Power Tool Housing Factory reveal that laboratory test results often diverge from actual production reality. Standard ISO test bars evaluate materials under ideal, static conditions. In contrast, complex power tool housing geometries introduce intricate flow paths, varying wall thicknesses, and internal residual stresses. Therefore, an engineering polymer that passes tensile and Izod impact tests in a laboratory can still fail catastrophic drop tests on the factory floor. Achieving true component reliability requires looking beyond isolated resin specifications and understanding how processing dynamics alter material morphology from sample prototyping to high-volume production. The Micro-Morphology Gap: 3 Processing Variables Dictating Real-World Reliability To bridge the gap between laboratory expectations and mass production performance, manufacturing engineers must analyze the internal micro-structure of molded polyamide parts. Three critical processing parameters directly dictate whether a PA6 GF30 component meets field durability targets. First, mold temperature controls the crystallization kinetics of the polyamide matrix. When injection molders run tools at excessively low temperatures to shorten cycle times, the outer polymer layer cools too rapidly. This rapid quenching creates an amorphous outer skin with high internal tension and lower molecular order. Conversely, maintaining an elevated mold temperature allows the polymer chains to align into dense, uniform crystalline structures. Proper crystallization enhances surface hardness, creep resistance, and dimensional stability, preventing premature shell cracking under localized loads. Second, fiber orientation and weld-line dynamics govern directional mechanical strength. As molten PA6 GF30 flows through intricate mold channels, the rigid glass fibers align parallel to the melt stream. While this anisotropic orientation boosts longitudinal tensile strength, it leaves transverse planes vulnerable to mechanical failure. Furthermore, where two melt fronts converge around internal ribs or screw bosses, they form weld lines. If the melt temperature or injection pressure drops at these confluence points, glass fibers fail to bridge the interface. As a result, weld lines become structural weak points that fracture easily during sudden dynamic drops. Third, moisture absorption fundamentally transforms the mechanical profile of polyamide 6. In its dry-as-molded state, PA6 GF30 exhibits maximum stiffness and tensile strength but remains relatively brittle under sharp impacts. Over time, ambient atmospheric moisture penetrates the polyamide matrix, breaking internal hydrogen bonds and acting as a natural plasticizer. This moisture conditioning process shifts the glass transition temperature downward, significantly improving impact energy absorption while slightly lowering flexural modulus. Ignoring post-molding moisture equilibrium often causes engineers to misinterpret initial quality control test results. Root Cause Engineering Case Study: Resolving Unexpected Drop-Test Failures in Production A practical engineering case illustrates how processing optimization resolves real-world structural failures. A major power tool manufacturer encountered severe shell fracturing near the battery latching mechanism during pre-production testing. The tool shell utilized a standard PA6 GF30 formulation, and initial material certification sheets confirmed full compliance with mechanical standards. Nevertheless, test units consistently cracked when dropped from a height of 1.5 meters onto concrete surfaces. Rather than immediately switching to a costlier resin grade, the engineering team conducted a comprehensive root cause failure analysis. Cross-sectional micro-imaging revealed significant fiber shear degradation and micro-void formation near the thin-walled battery housing section. High injection speeds had generated excessive melt shear, fracturing long glass fibers into short fragments and reducing their reinforcing efficiency. Additionally, sub-optimal mold temperature distribution caused uneven cooling rates across asymmetric wall sections, resulting in internal warping stresses. The engineering team implemented a multi-stage corrective action plan. First, they optimized the injection velocity profile to minimize fiber attrition during gate passage. Second, they adjusted mold cooling channels to balance surface temperatures within an optimal window of 85°C to 95°C. Finally, they refined the gate location to move the primary melt front convergence away from high-stress structural ribs. Without altering the mold cavity geometry or changing the underlying resin specification, these process refinements increased the energy absorption capability of the housing by over 40%, completely eliminating drop-test failures during mass production runs. BOCHENG’s PA6 GF30 Engineering Solutions: Bridging Material Synthesis and Processing Control Solving complex manufacturing challenges demands raw materials formulated specifically for broad processing windows and consistent melt behavior. Material innovation from BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd.) directly addresses these production realities. By optimizing polymer chain length distribution and incorporating advanced glass fiber coupling agents, the company manufactures high-performance PA6 GF30 injection-grade materials in both natural and black options. These formulations deliver exceptional melt flow fluidity, superior fiber-matrix interfacial bonding, and minimal batch-to-batch viscosity fluctuation. Furthermore, the technical team at Xiamen Bocheng Plastic Materials Co., Ltd. recognizes that high-quality resin represents only half of the reliability equation. The enterprise provides comprehensive technical support to molders and OEMs, offering mold flow simulation assistance, thermal process optimization parameters, and post-injection conditioning guidelines. Beyond power tool enclosures, these engineering resins support demanding automotive and industrial parts manufacturing applications where structural integrity remains non-negotiable. By combining tailored material chemistry with practical processing expertise, BOCHENG ensures that client components retain their mechanical integrity from initial prototype sampling through millions of production cycles. Strategic Takeaways: How Global OEMs Can Guarantee Housing Durability from Day One Ensuring long-term product reliability in demanding market sectors requires a shift in procurement and engineering mindset. Original equipment manufacturers can no longer evaluate raw material value based solely on unit price per kilogram or static data sheet metrics. Instead, successful brand owners focus on total yield efficiency, processing consistency, and real-world part performance under dynamic stress. Establishing close technical collaboration between material compounders, tool designers, and injection molding facilities early in the product development lifecycle mitigates costly design revisions. When compounders provide precise melt rheology data and processing support, molders can eliminate internal stress concentrations, optimize fiber orientation, and control moisture conditioning effectively. Ultimately, mastering the interplay between material synthesis and molding parameters allows manufacturers to produce lighter, stronger, and safer power tool housings. Through rigorous quality management system certifications and specialized compounding technology, advanced material partners help global brands overcome mass-production hurdles and secure a competitive advantage in global markets. To explore specialized PA6 GF30 material grades and technical engineering support, visit https://www.pa6-pa66.com/.
Read More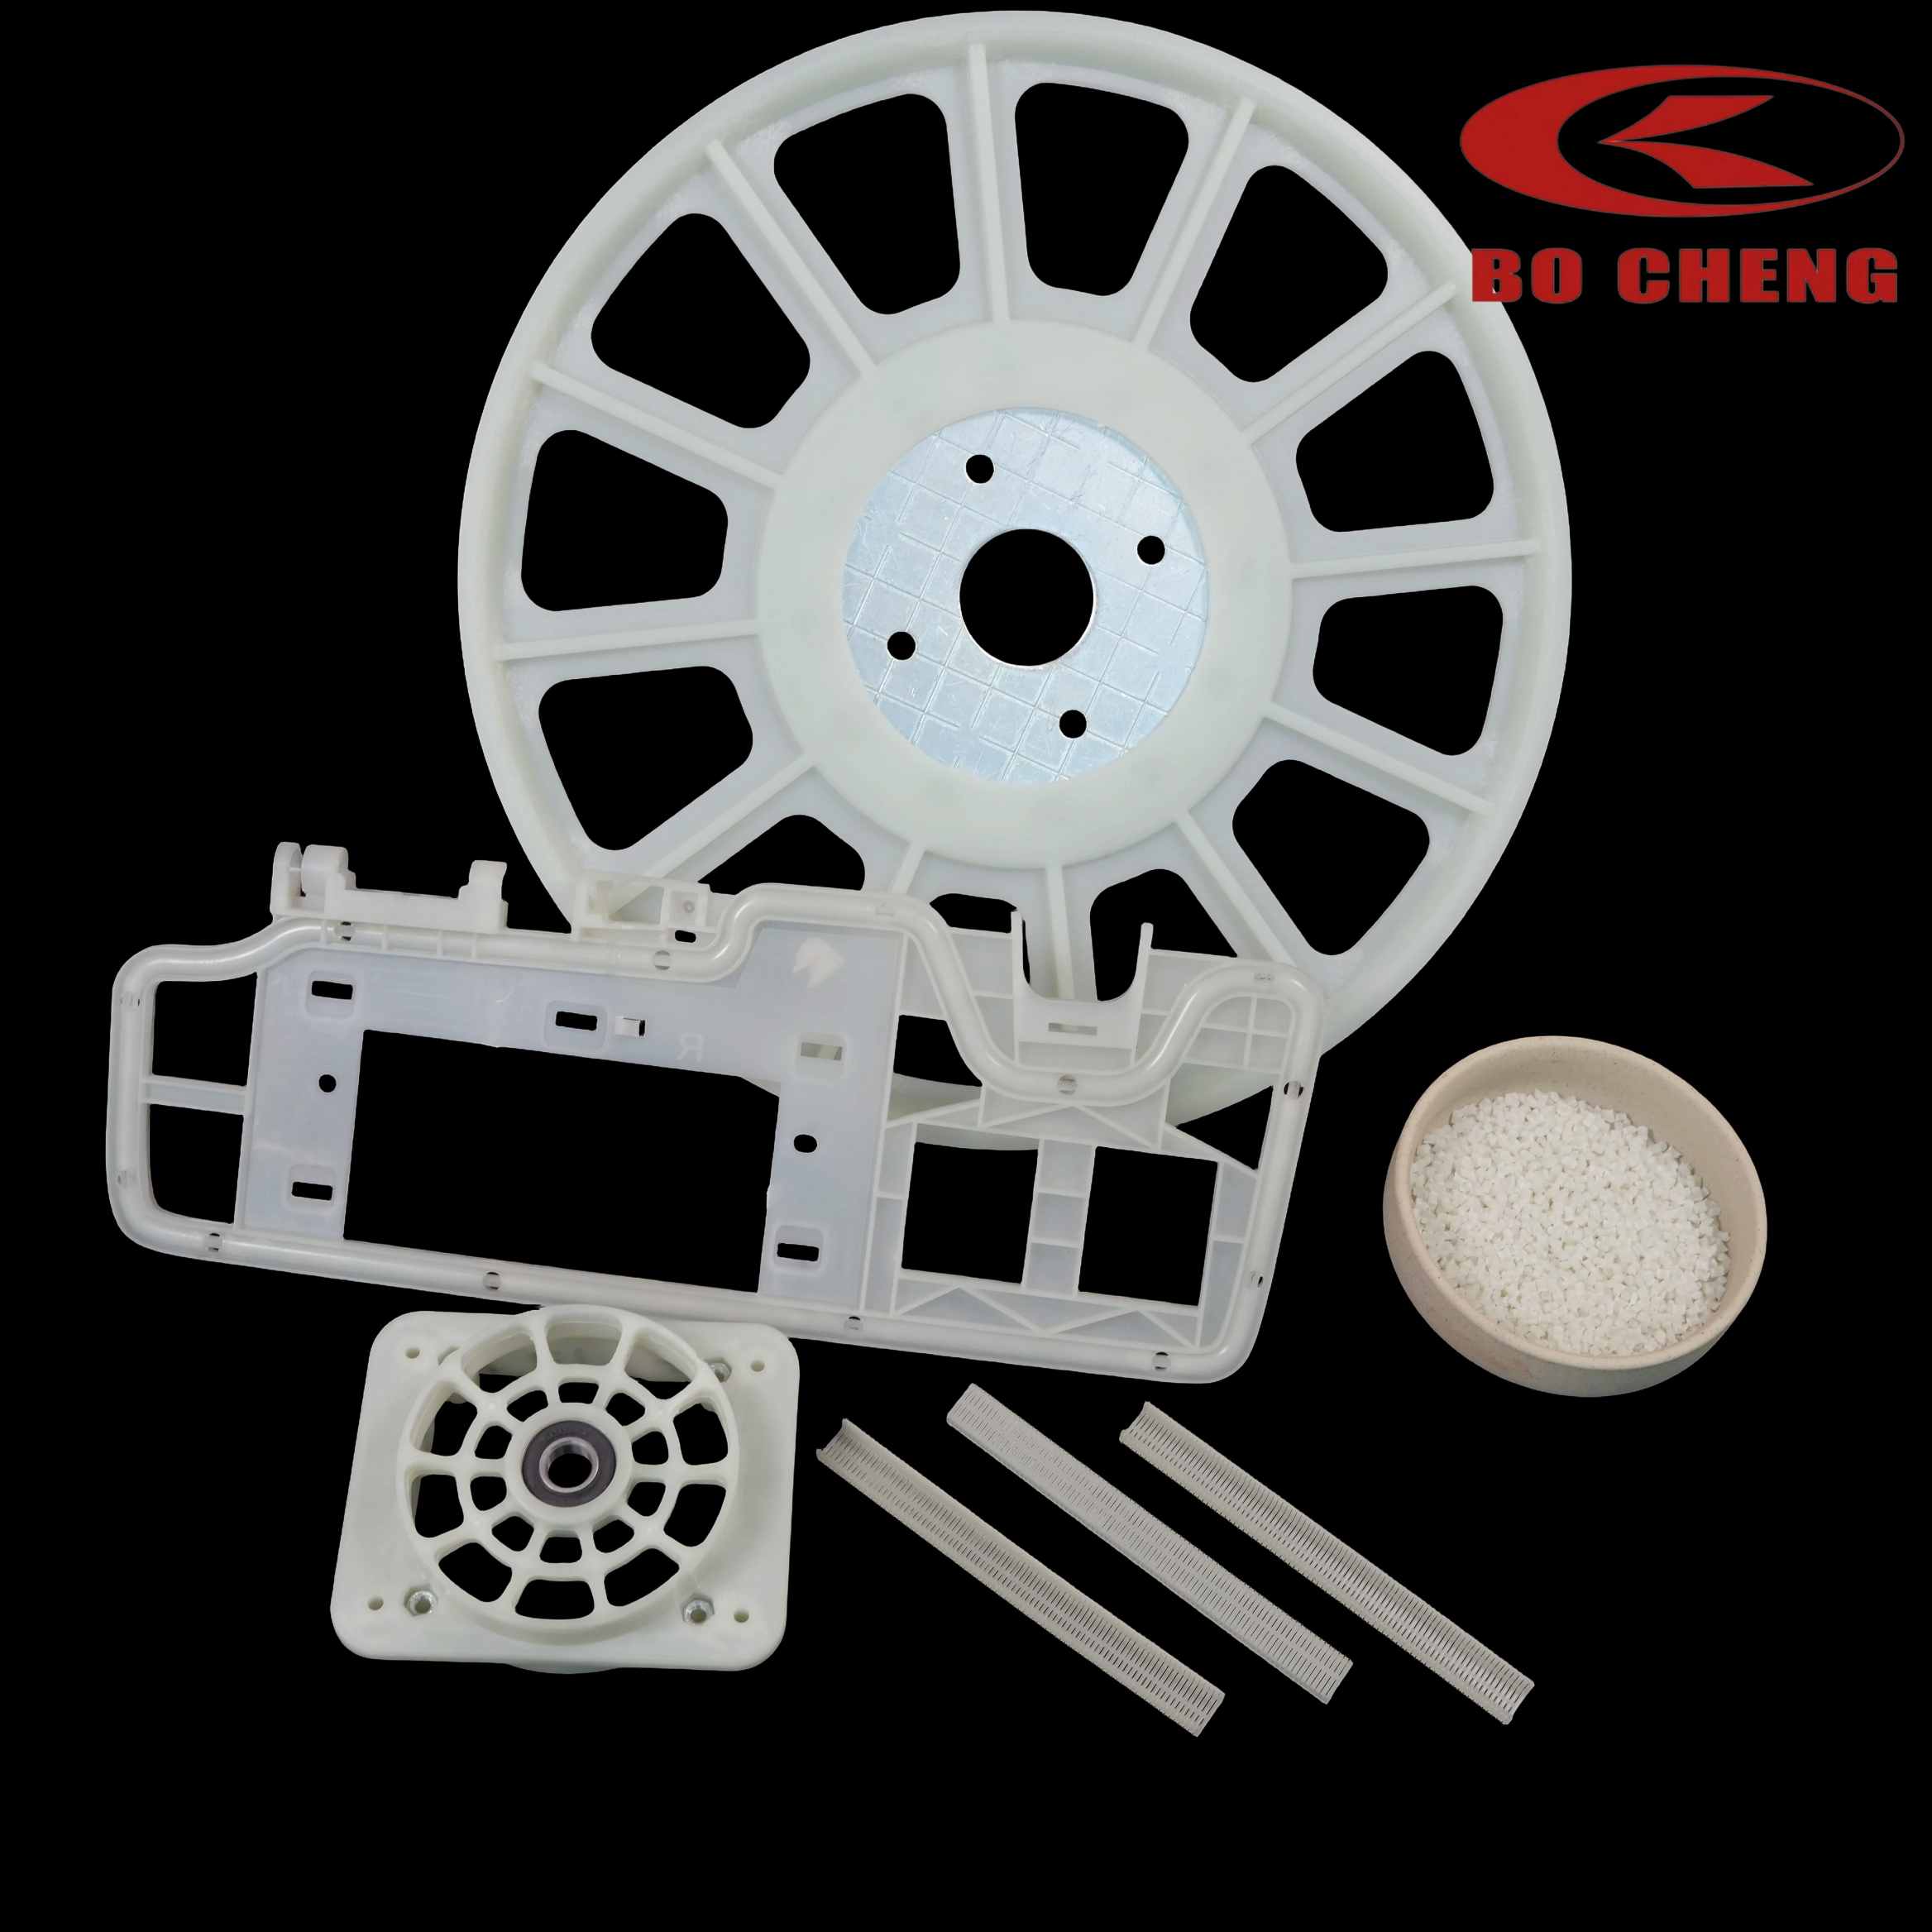
Industrial manufacturing faces continuous price shifts in polymer raw materials. Fluctuations in upstream feedstocks, such as Caprolactam for Polyamide 6 (PA6) and Adiponitrile for Polyamide 66 (PA66), directly impact global engineering supply chains. Design teams must select polymers that offer structural reliability without driving up production budgets. As a certified High Quality 30% Glass Fiber Reinforced Nylon 6 Supplier, industry experience demonstrates that material selection requires a balance between thermal limits, mechanical load, and procurement costs. Replacing over-specified materials with economically viable alternatives requires thorough technical evaluation. Engineers who analyze specific operating environments can prevent premature field failures while reducing unnecessary material expenses. Raw Material Volatility and the Strategic Trade-Off in Polyamide Selection Global supply chain dynamics continually force engineering teams to re-evaluate polymer choices. Caprolactam, the primary precursor for PA6, features a broad global supplier base and relatively stable production economics. Conversely, Adiponitrile and hexamethylenediamine, essential feedstocks for PA66, experience frequent supply bottlenecks and sharper cost spikes. Consequently, procurement costs for PA66 resins remain higher and less predictable than those for PA6. However, selecting an engineering resin solely based on unit price creates hidden risks during long-term operation. Over-specifying a component by defaulting to PA66 GF30 when PA6 GF30 satisfies all mechanical requirements adds unnecessary costs across high-volume production cycles. Conversely, under-specifying a material in high-temperature environments leads to thermal deformation and system failure. Achieving long-term profitability and component integrity demands an objective selection framework based on empirical testing data rather than traditional procurement habits. The Comparative Selection Matrix: PA6 GF30 vs. PA66 GF30 Evaluating 30% glass fiber reinforced polyamides requires an analysis of core physical parameters under identical test conditions. Incorporating 30% short glass fibers into polyamide matrix resin significantly raises tensile strength, flexural modulus, and heat deflection temperatures compared to neat polymers. However, structural differences between the PA6 and PA66 polymer chains create distinct performance profiles. Mechanical Strength and Modulus Metrics Both PA6 GF30 and PA66 GF30 exhibit impressive mechanical baseline properties. Typical tensile strength values for these compounds range between 140 MPa and 185 MPa in the dry-as-molded state. Similarly, flexural modulus values fall between 8,500 MPa and 9,500 MPa. While PA66 GF30 retains slightly higher rigidity at elevated temperatures, PA6 GF30 demonstrates comparable load-bearing capabilities under standard ambient operating conditions. Thermal Deflection and Heat Aging Resistance Thermal capabilities represent a primary technical separator between the two polyamides. Under a heavy mechanical load of 1.8 MPa, PA66 GF30 typically achieves a Heat Deflection Temperature (HDT) of approximately 245°C to 250°C. In comparison, PA6 GF30 offers an HDT range between 205°C and 215°C. For continuous operating temperatures exceeding 150°C, PA66 GF30 maintains structural integrity over long durations. Nonetheless, PA6 GF30 provides reliable thermal performance for intermediate temperature envelopes below 130°C. Moisture Absorption and Dimensional Behavior Hydrodynamics significantly influence long-term dimensional stability. PA6 contains a higher density of amide groups per carbon chain length than PA66, resulting in higher moisture absorption rates. At equilibrium in standard atmospheric environments, PA6 GF30 absorbs approximately 2.5% to 3.0% moisture by weight, whereas PA66 GF30 absorbs roughly 1.8% to 2.2%. Moisture intake acts as a plasticizer, slightly lowering mechanical strength while increasing impact resistance. Engineers must account for post-molding shrinkage and moisture expansion when designing precision components with tight tolerance requirements. Rheology and Processing Window Differences Processing characteristics directly influence manufacturing cycle times and mold longevity. PA6 features a lower melting point around 220°C and lower melt viscosity compared to PA66, which melts near 260°C. The higher fluidity of PA6 GF30 allows injection molders to operate at lower barrel temperatures and reduced injection pressures. Consequently, PA6 GF30 flows smoothly into intricate mold cavities and thin-walled geometry, reducing energy consumption and minimizing tool wear over high-volume production runs. Engineering Decision Tree: Application Scenarios & Operating Envelopes Mapping material properties to real-world operational demands clarifies the decision-making process. Component designers should evaluate three primary factors: peak operating temperature, continuous mechanical exposure, and total production volume. Automotive Engineering Applications Automotive structural design relies heavily on reinforced polyamides to achieve weight reduction and durability. In high-heat engine compartments, PA66 GF30 serves as the preferred resin for intake manifolds, engine covers, and radiator end tanks, where exposure to continuous ambient heat exceeds 140°C. Conversely, PA6 GF30 excels in exterior structural brackets, door handle assemblies, and pedal modules. Furthermore, PA6 GF30 provides superior surface appearance, eliminating fiber read-through on visible components while reducing injection molding cycle times. Specialized compounds find extensive utility across automotive and industrial parts manufacturing environments. Industrial Equipment and Power Tools Industrial equipment components, such as gear housings, belt pulleys, handles, and electrical enclosures, operate under continuous dynamic stress. PA66 GF30 provides necessary rigidity for heavy-duty drive gears subjected to high continuous frictional heat. However, PA6 GF30 offers superior energy absorption upon impact, making it ideal for hand-held power tool casings and structural housings exposed to drop risks and vibration. Home Appliances and Consumer Products Washing machine structural frames, pump housings, and internal support brackets benefit greatly from the cost profile of PA6 GF30. Because internal appliance temperatures rarely exceed 90°C, PA6 GF30 fulfills structural stiffness and creep resistance requirements without adding unnecessary resin costs. The Cost-to-Performance Evaluation Rule Engineers can successfully transition from PA66 GF30 to PA6 GF30 when maximum operating temperatures remain below 130°C and dimensional tolerance windows allow for minor moisture relaxation. This substitution reduces resin procurement costs by 15% to 25% while maintaining critical structural safety margins. Tailored Compounding Solutions: How BOCHENG Optimizes Polyamide Performance Navigating material selection requires experienced compounding partners who understand raw polymer behavior and glass reinforcement mechanics. Advanced processing techniques allow custom compounding specialists to bridge performance gaps between standard PA6 and PA66 formulations. Precision Glass Fiber Dispersion The technical team at BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd) utilizes twin-screw compounding systems equipped with specialized screw configurations. This equipment ensures uniform glass fiber distribution while preserving optimal glass fiber length retention within the polymer matrix. Superior fiber-matrix adhesion maximizes tensile modulus and impact performance, ensuring consistent lot-to-lot structural reliability. Customized Property Modifications Standard resin grades cannot solve every engineering challenge. Custom compounding capabilities enable the addition of specialized property modifiers: l Heat aging stabilizers to extend continuous working temperatures in thermal environments. l Flame retardant packages compliant with UL94 V-0 safety standards. l Hydrolysis-resistant additives for long-term exposure to automotive coolants and hot water. l UV stabilizers and custom color matching to meet precise aesthetic specifications. Rigorous Quality Management and Compliance Maintaining consistent quality requires strict operational controls. Xiamen Bocheng Plastic Materials Co., Ltd operates under ISO 9001 and IATF 16949 quality management frameworks. Every batch undergoes comprehensive laboratory testing, including melt flow indexing, tensile testing, ash content analysis, and moisture determination. Raw materials comply fully with RoHS and REACH environmental regulations, providing global manufacturers with total compliance assurance. Conclusion: Partnering with BOCHENG for Optimal Material Value Choosing between PA6 GF30 and PA66 GF30 involves a balanced evaluation of thermal exposure, mechanical demands, and economic objectives. While PA66 GF30 remains indispensable for extreme thermal conditions, PA6 GF30 presents an exceptionally efficient solution for a vast majority of structural applications across the automotive, industrial, and appliance sectors. Strategic material selection enables engineering teams to optimize component performance without exceeding budgetary constraints. By partnering with experienced compounding experts, OEMs and tier-1 suppliers gain access to tailored resin formulations, comprehensive technical datasheets, and reliable global delivery schedules. To review detailed material technical data sheets, request custom sample formulations, or schedule a cost-optimization engineering evaluation, visit https://www.pa6-pa66.com/.
Read More
Modern electrical architectures demand rigorous thermal stability, mechanical strength, and reliable fire safety standards. As miniaturization accelerates across consumer electronics, industrial switchgear, and energy distribution networks, internal operating temperatures rise significantly. Design engineers face growing pressure to select structural materials that withstand high heat without compromising structural integrity or electrical insulation. Evaluating specialized engineering thermoplastics becomes essential to prevent thermal runaways, short circuits, and catastrophic fire hazards. Selecting a trustworthy material supplier is paramount in this engineering process. Working alongside a recognized High Quality PA66 GF30 FR V0 Supplier provides electrical equipment manufacturers with crucial technical guidance, verified flame retardancy, and consistent compound quality. Consequently, comprehensive material selection guides now serve as vital engineering benchmarks. These guides effectively bridge global safety directives with practical manufacturing considerations across diverse industrial markets worldwide. Regulatory Evolution: Driving the Shift Toward Eco-Friendly & Flame-Retardant Polyamides International safety frameworks continuously adapt to higher environmental and operational standards. Regulatory directives such as IEC 60335 for household appliances and UL 60950/62368 for information technology equipment enforce strict flammability rules. Historically, component manufacturers relied heavily on halogenated flame retardants due to their cost efficiency and effective gas-phase flame suppression mechanisms. However, halogen-based additives release toxic, corrosive fumes during combustion. These emissions create significant health and environmental risks during thermal breakdown or accidental structural fires. In response, modern regulatory updates, aligned with European Union RoHS and REACH directives, strongly incentivize halogen-free flame retardant (HFFR) systems. Modern HFFR technology relies on phosphorus, nitrogen, or inorganic mineral mechanisms to control combustion effectively. These advanced formulations form protective carbonaceous char layers during thermal exposure, which effectively cut off oxygen access and reduce hazardous smoke density. Polyamides modified with these eco-friendly additives fulfill stringent environmental compliance mandates while retaining exceptional dielectric strength and volume resistivity. Therefore, transitioning toward sustainable flame-retardant polyamide compounds represents both a regulatory obligation and a strategic performance advantage for forward-thinking electrical component manufacturers worldwide. Decoding UL94 V0 Compliance: Technical Test Criteria for High-Safety Enclosures Understanding flame retardancy requires a detailed look at international testing metrics, primarily the UL94 standard published by Underwriters Laboratories. The UL94 V0 rating represents one of the highest vertical burning safety classifications achievable for solid plastic compounds. During standardized laboratory testing, technicians subject vertically clamped bar specimens to controlled burner flames for two sequential 10-second applications. To achieve a V0 classification, individual afterflame combustion times (t1 and t2) must not exceed 10 seconds. Furthermore, the total accumulated afterflame time for five test specimens across ten ignitions must remain strictly under 50 seconds. Crucially, test specimens must produce zero flaming drips that could ignite the surgical cotton placed directly beneath the testing apparatus. Beyond basic UL94 flammability ratings, advanced electrical safety protocols evaluate the Glow Wire Flammability Index (GWFI) and Glow Wire Ignition Temperature (GWIT) according to IEC 60695 specifications. A high GWFI score, such as 960 degrees Celsius, confirms that the polymer self-extinguishes rapidly after direct contact with an electrically heated wire element. Similarly, a high GWIT score ensures that hot internal components do not initiate open flames during unexpected electrical overload conditions. These rigorous test criteria give design engineers absolute confidence when selecting materials for unattended electrical housing units. The Engineering Synergy: Balancing 30% Glass Fiber Reinforcement with Flame Retardancy Achieving fire safety alone is insufficient for demanding structural electrical housings. Outer casings, terminal blocks, and internal supports must endure mechanical vibrations, physical impacts, and continuous thermal stress during daily operation. Integrating 30% short glass fibers into Polyamide 66 matrix creates a formidable engineering compound known as PA66 GF30. Glass fiber reinforcement increases tensile strength, flexural modulus, and dimensional stability by a substantial margin. Additionally, it elevates the Heat Deflection Temperature (HDT) under heavy load, allowing structural components to perform reliably in operating environments exceeding 150 degrees Celsius. However, glass fiber insertion introduces a complex physical phenomenon known as the candlewicking effect. Fibers exposed at the material surface during burning can draw molten polymer upward through capillary action, continually feeding the flame and threatening combustion control. Advanced compounding techniques solve this challenge through precise additive dispersing, optimizing char formation to encapsulate glass fibers during flame exposure. Furthermore, modern PA66 GF30 FR V0 formulations carefully preserve the Comparative Tracking Index (CTI), typically maintaining performance ratings above 600 volts. This exceptional dielectric property prevents electrical arcing across conductive surface tracks, striking an ideal balance between mechanical stiffness, flame resistance, and high-voltage insulation reliability. Real-World Benchmarks: Component-Specific Material Requirements Electrical components operate under diverse physical stress conditions, necessitating tailored material properties across different device architectures. In high-density terminal blocks and multi-pin connectors, thin-wall flame retardancy becomes critical. Materials must achieve certified UL94 V0 ratings at wall thicknesses down to 0.8 millimeters or 1.6 millimeters without warping or losing dimensional precision. Precise melt flowability during precision injection molding ensures complete filling of intricate mold geometries, preventing internal voids or structural weak points in critical component walls. For miniature circuit breakers (MCBs) and molded case circuit breakers (MCCBs), outer housings must withstand sudden thermal shocks, mechanical recoil, and internal arc flashes. Mechanical structural integrity must remain fully intact during high-current fault conditions to prevent catastrophic casing rupture. Moreover, structural components deployed in automotive and industrial parts manufacturing require exceptional resistance to automotive fluids, industrial chemicals, and broad operational temperature swings ranging from -40 degrees Celsius to over 150 degrees Celsius. Meeting these demanding benchmarks demands consistent raw polymer sourcing, stringent compounding quality control, and deep material processing expertise across all production stages. BOCHENG’s PA66 GF30 FR V0: Tailored Compound Solutions & Technical Partnership Meeting these demanding technical specifications requires close collaboration with experienced engineering material compounders. BOCHENG(Xiamen Bocheng Plastic Materials Co., Ltd) has established itself as a leading innovator in modified engineering thermoplastics. The enterprise specializes in high-performance PA6, PA66, and specialty flame-retardant formulation technologies, delivering premium material solutions engineered specifically for demanding industrial environments. Through meticulous formulation development and rigorous testing, BOCHENG ensures that its PA66 GF30 FR V0 materials deliver consistent mechanical strength, verified flame ratings, and superior thermal endurance batch after batch. In addition to standardized material grades, Xiamen Bocheng Plastic Materials Co., Ltd offers customized compounding services designed to meet specialized application requirements. The engineering team actively assists original equipment manufacturers (OEMs) and injection molders with custom color matching, rheology modification, and processing parameter optimization. Furthermore, BOCHENG provides comprehensive technical testing support, helping clients streamline their product verification and international certification processes. By maintaining strict quality assurance protocols and utilizing advanced twin-screw extrusion technologies, BOCHENG delivers reliable compound solutions that empower global manufacturers to build safer, more durable electrical assemblies. Conclusion Electrical housing safety relies on a holistic design approach that combines regulatory compliance, precise flame resistance testing, and optimized mechanical engineering. Polyamide 66 reinforced with 30% glass fiber and modified with certified V0 flame retardants provides an unmatched balance of physical strength, thermal endurance, and high-voltage electrical safety. Partnering with a dedicated compound manufacturer enables electrical equipment developers to navigate evolving global standards with complete confidence. To explore high-performance modified plastics, detailed technical datasheets, and custom compounding options, visit the official enterprise portal at https://www.pa6-pa66.com/.
Read More
Selective Laser Sintering (SLS) technology has fully transitioned from rapid prototyping into mainstream industrial manufacturing. As production volumes expand across automotive, consumer electronics, aerospace, and medical device sectors, service providers face pressing economic and logistical demands. In large-scale industrial build environments, raw material expenditure accounts for up to forty percent of total component production costs. Original equipment manufacturer (OEM) polyamide 12 (PA12) powders often impose substantial operational costs and rigid delivery schedules. Consequently, enterprise operators actively evaluate alternative material options to protect margin performance and ensure supply continuity. Identifying a Reliable Custom EOS PA12 Powder Alternative Supplier has therefore become a strategic priority for additive manufacturing bureaus worldwide. This material diversification movement reflects broader trends in global supply chain management. Production facilities require raw material sources that deliver uncompromised mechanical properties while offering scalable pricing models. Furthermore, global geopolitical shifts and logistics bottlenecks highlight the risk of relying on single-source material streams. By qualifying specialized third-party polymer compounders, manufacturing operations gain greater cost flexibility and localized support without sacrificing equipment uptime. Industrial users increasingly demand stable, high-purity polymer formulations capable of matching OEM performance metrics across demanding multi-day print runs. Furthermore, expanding operational capacity requires seamless material integration across existing machinery fleets. Manufacturing plants must maintain continuous throughput without requiring expensive hardware modifications or prolonged calibration cycles. As a result, material engineering teams carefully analyze physical powder dynamics to guarantee seamless drop-in performance. Key Technical Benchmarks for EOS-Compatible Alternative PA12 Powders How do technical managers evaluate whether a third-party powder matches original EOS platform standards? The answer lies in precise physical particle characteristics, chemical purity, and thermal behavior during laser sintering. First, particle size distribution (PSD) governs powder recoating behavior and final surface roughness. High-performance powders maintain tight dimensional boundaries. For optimal packing density and smooth layer deposition, D10 values typically range between 25 and 30 microns. D50 median particle sizes sit between 45 and 50 microns, while D90 values remain controlled between 70 and 75 microns. When fine particles below 20 microns accumulate, inter-particle van der Waals forces trigger powder agglomeration during recoating. Conversely, oversized particles above 80 microns cause surface streaking and decrease sintered part density. Maintaining a uniform spherical morphology further reduces internal friction, yielding an angle of repose around 32 degrees for seamless recoater blade passes. Second, thermal stability defines the sintering window during printer operation. Polyamide 12 requires a broad thermal differential between its melting point and crystallization temperature. A standard formulation displays a melting point between 178 and 183 degrees Celsius and a crystallization point between 145 and 155 degrees Celsius. This broad processing window, spanning 20 to 30 degrees Celsius, prevents premature crystallization when bed temperatures operate between 165 and 175 degrees Celsius. Stable thermal behavior prevents warping, curling, and layer delamination during long production builds. Finally, recyclability determines long-term cost viability in commercial 3D printing applications. Reliable alternative powders sustain consistent molecular weight and melt flow rate across multiple build cycles. Service bureaus regularly operate with refresh ratios between 30 percent and 70 percent new powder. In addition, moisture content must remain strictly below 0.10 percent by weight to prevent bubble formation, surface degradation, or inconsistent laser absorption. Careful monitoring of thermal degradation over time ensures that recycled fractions preserve mechanical integrity in finished components. Polymer Engineering Heritage: The Foundation of Batch Consistency Why does deep polymer compounding experience matter when selecting an SLS material manufacturer? Grinding raw polymer pellets into fine powder represents only one stage of the production cycle. True material reliability requires comprehensive control over polymer chemistry, melt stabilization, and micro-particle morphology. Companies with an extensive background in thermoplastic engineering bring distinct advantages to additive manufacturing. For instance, BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd.) leverages over 17 years of experience in specialized polymer modification and compounding. Rather than acquiring generic secondary powders, technical teams engineer base formulations using twin-screw compounding systems. This melt-compounding stage evenly disperses heat stabilizers, anti-oxidants, and flow aids at the molecular level. This fundamental engineering approach ensures that the base resin maintains structural integrity under repeated laser exposure. To preserve polymer chain integrity during size reduction, specialized processors utilize cryogenic freezing systems. Processing material at temperatures down to minus 100 degrees Celsius prevents thermal degradation and maintains uniform spherical particle shapes. Advanced air classification systems then remove satellite fines and oversized particles, resulting in a predictable particle size distribution curve. Quality control protocols further reinforce batch-to-batch predictability. Certified under ISO 9001 and IATF 16949 quality management frameworks, BOCHENG enforces a five-stage quality control system. Quality assurance teams inspect raw polymer feeds, modified pellets, raw milled powder, thermal DSC profiles, and final Certificate of Analysis (COA) metrics. This systematic oversight ensures that every production batch behaves predictably inside industrial EOS laser sintering systems. Tailored Solutions and Commercial Flexibility with BOCHENG BC-PA12-S01 What specific material attributes and commercial options support specialized end-use applications? Industrial applications often demand properties beyond standard white prototype parts. The flagship formulation, designated as BC-PA12-S01, provides high mechanical toughness, chemical resistance, and thermal stability. Sintered components achieve a tensile strength of approximately 46 MPa, along with exceptional resistance to water, oils, alkalis, and fuels. These physical properties render the material suitable for functional automotive ducts, electronic enclosures, and durable industrial tooling. Long-term environmental resistance ensures that finished components maintain structural stability under demanding field conditions. Beyond standard grade specifications, BOCHENG provides extensive customization capabilities. Customers can request specific particle size distributions, tailored mesh ranges, and custom color options including deep black and neutral gray. For demanding structural applications, the product matrix includes glass-fiber-reinforced variants like BC-PA12-GF-S01, carbon-fiber-filled options like BC-PA12-CF-S01, as well as PA11 and flexible TPU 90A powders. Commercial flexibility forms another pillar of industrial supply support. Xiamen Bocheng Plastic Materials Co., Ltd. accommodates low minimum order quantities starting at 25 kilograms in moisture-proof bags or heavy-duty drums. Direct access to international shipping routes via Xiamen Port enables prompt global delivery, allowing service bureaus to maintain lean material inventories while responding rapidly to client project demands. Flexible purchasing structures allow prototyping houses and large contract manufacturers to scale procurement seamlessly in response to fluctuating build volumes.
Read More
Recent international aerospace exhibitions and industrial drone expos clearly demonstrate a major material shift in unmanned aerial vehicle (UAV) design. Modern platforms for agricultural spraying, infrastructure inspection, and aerial mapping demand structural components that combine low density with exceptional rigidity. Traditional aluminum alloys and standard unreinforced plastics can no longer satisfy the strict requirements of continuous outdoor operations. Material scientists and airframe engineers increasingly turn to advanced polymer composites to solve these challenges. A thorough evaluation of flight dynamics and environmental exposure explains why Nylon Dominates Drone Arm and Airframe Manufacturing across the commercial drone sector. By combining specialized long-chain polyamides with high-modulus carbon fibers, material developers have set a new standard for structural stiffness, dynamic fatigue resistance, and dimensional stability in high-stress UAV components. The Environmental and Mechanical Challenges of Modern Drone Airframes Industrial multirotor drones operate under continuous mechanical forces and harsh weather conditions that test airframe materials to their physical limits. Drone arms must support heavy payloads, including optical sensors, LIDAR units, and agricultural liquid tanks, while enduring aerodynamic turbulence and rapid maneuvers. At the same time, high-speed motor rotation generates intense high-frequency vibrations that transfer directly into the arm structure. Over hundreds of operational hours, these cyclic vibrational loads induce stress concentration at connection points, causing micro-cracks and structural fatigue in standard materials. Environmental exposure creates another major operational obstacle for drone components. Agricultural drones frequently work in humid environments and pesticide mists, while coastal inspection drones face salt spray and high relative humidity. Conventional short-chain polyamides, such as standard PA6 and PA66, contain a high concentration of polar amide groups along their polymer backbones. These hydrophilic groups readily absorb atmospheric moisture, reaching saturation levels between 2.5% and 8.5%. Absorbed water molecules act as plasticizers inside the polymer matrix, which reduces tensile strength and flexural modulus by up to 50%. Furthermore, moisture absorption leads to dimensional expansion and distortion. Even a minor arm misalignment shifts motor geometry, forcing flight controllers to consume extra battery power to compensate. Molecular Superiority: Why PA612 Base Resin Delivers Low Moisture Absorption and High Stability To eliminate moisture-induced degradation, material engineers selected Polyamide 612 (PA612) as the primary matrix resin for demanding airframe structures. The molecular architecture of PA612 features longer methylene carbon chains separating its amide functional groups. This long-chain structure reduces the spatial density of polar amide groups along the polymer backbone, giving the base resin significant hydrophobic properties. Laboratory measurements confirm that PA612 exhibits a saturated water absorption rate of less than 0.5%, representing a major improvement over standard PA6 and PA66 polymers. As a result, parts molded from PA612 retain their mechanical stiffness, impact resistance, and precise dimensions regardless of atmospheric humidity or direct liquid contact. When integrated into drone arms, PA612 maintains accurate motor alignment and structural geometry across changing environmental conditions. The long-chain resin also offers excellent chemical resistance against fertilizers, solvents, and fuels. In addition, the inherent flexibility of long methylene chains provides strong energy absorption, allowing drone arms to absorb landing impacts and resist cyclic flexural stress during flight. CF30 vs. CF40: Strategic Selection Between Structural Rigidity and Mold Flowability Unreinforced PA612 provides an exceptionally stable base, but heavy-duty drone structures require higher stiffness to prevent flexure under maximum rotor thrust. Compounding PA612 with short carbon fibers creates a lightweight, ultra-rigid composite that effectively replaces aluminum alloys and composite tubing. Design engineers typically evaluate two primary reinforcement levels for airframe components: 30% carbon fiber (CF30) and 40% carbon fiber (CF40). Choosing between CF30 and CF40 involves balancing mechanical stiffness requirements against polymer flow during injection molding. PA612 CF30 offers a balanced combination of tensile strength, flexural modulus, and processing ease. The 30% fiber loading increases structural stiffness substantially while maintaining good melt flow. This grade enables manufacturers to produce complex geometries with thin walls, internal reinforcement ribs, and snap-fit features without creating excessive internal stress or surface defects. In contrast, PA612 CF40 maximizes flexural rigidity and tensile performance, making it the ideal choice for long-span arms on heavy-lift drones. The 40% carbon fiber loading achieves a flexural modulus that rivals light metals, virtually eliminating structural flexure during flight. However, higher fiber content increases melt viscosity and flow resistance during molding. Engineers must evaluate part geometry and structural loads carefully when choosing between these two compounds. Overcoming Injection Molding Hurdles in Long-Span Carbon-Nylon Components Processing carbon-reinforced PA612 into finished drone components requires precise thermal and mechanical management during injection molding. Carbon fiber-filled polymers exhibit distinct flow behavior inside the mold cavity. As the molten compound flows through gates and runners, carbon fibers align primarily along the direction of flow. This orientation creates anisotropic mechanical properties and differential shrinkage rates between parallel and perpendicular flow directions. Uncontrolled anisotropic shrinkage can cause part warpage and internal stress in long drone arms. Processing technicians optimize mold temperature, injection velocity, and holding pressure to control fiber orientation and ensure uniform packing. Maintaining appropriate mold temperatures keeps the polymer matrix fluid long enough to achieve thorough packing, which reduces surface defects such as fiber floating. In addition, plasticizing equipment must use gently designed screws to minimize fiber breakage. Preserving fiber length maintains a higher aspect ratio, which directly protects the final strength of the molded airframe. BOCHENG Engineering Solutions: Tailored PA612-CF Compounds and Technical Support for Aerospace Applications Meeting the strict mechanical requirements of commercial drone manufacturing demands specialized compounding expertise and reliable material quality. Advanced material suppliers, such as BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd), supply high-performance carbon fiber reinforced polyamides to international drone OEMs. Using twin-screw extrusion technology and specialized chemical coupling agents, BOCHENG ensures strong interfacial bonding between the PA612 resin matrix and short carbon fibers. Strong interfacial adhesion enables efficient stress transfer from the resin matrix to the carbon fibers during operation. This structural enhancement optimizes tensile strength, flexural rigidity, and fatigue endurance under continuous mechanical loads. BOCHENG customizes carbon fiber content, flow behavior, and flame retardancy to align with specific customer specifications and mold designs. Quality control remains central to material production. Lot-to-lot consistency and mechanical performance are verified through recognized international quality certifications, including ISO9001 and IATF16949 standards. These quality frameworks ensure that every batch of PA612-CF material meets exact standards for density, mechanical strength, and thermal resistance. Beyond compound supply, technical teams at Xiamen Bocheng Plastic Materials Co., Ltd assist customer engineers with mold flow analysis, FEA evaluations, and processing parameter optimization. This technical support speeds up product development and lowers tooling iteration costs for airframe manufacturers. As the commercial drone industry continues to grow across agriculture, inspection, and logistics, the demand for lightweight, high-strength structural materials will remain strong. The combination of PA612 long-chain polyamide and high-modulus carbon fiber provides a reliable material choice to eliminate moisture absorption, structural distortion, and fatigue failure. Material formulations developed by BOCHENG continue to support airframe innovation, enabling commercial drones to fly longer and operate reliably in demanding environments. For more details regarding carbon fiber reinforced nylon materials and technical solutions, visit https://www.pa6-pa66.com/.
Read More
Global manufacturing industries continuously seek advanced engineering materials to optimize structural efficiency and energy consumption. Traditional structural metals like die-cast aluminum, zinc alloys, and machined steel have long dominated critical mechanical applications. However, modern engineering requirements demand lighter structural materials that maintain high strength under severe thermal and mechanical loads. Engineering thermoplastics have stepped into this role, offering scalable high-volume processing through injection molding while drastically reducing component weight. Polyamide 66, commonly known as PA66, serves as a highly versatile base polymer due to its inherent mechanical toughness, chemical resistance, and elevated melting temperature. To bridge the performance gap between unfilled plastics and structural metals, compounders incorporate high-modulus carbon fibers into the resin matrix. Specially engineered grades like PA66 CF30 for Industrial Use represent a significant advancement in lightweight materials engineering. Incorporating 30% short carbon fiber by weight creates a high-performance composite material capable of replacing heavy metal alloys in demanding operational environments. Consequently, design engineers across multiple industrial sectors rely on modified polyamide solutions to meet aggressive performance goals. Q1: How Does 30% Carbon Fiber Reinforcement (CF30) Compare to Glass Fiber (GF30) in Mechanical Performance? To understand the mechanical advantages of PA66 CF30, engineers must examine the microstructural differences between carbon fibers and glass fibers. Both additives reinforce the host polymer matrix by transferring mechanical loads across fiber-matrix interfaces. However, carbon fiber possesses significantly higher intrinsic stiffness and lower physical density compared to standard E-glass fiber. Consequently, a 30% carbon fiber compound achieves superior mechanical properties while simultaneously lowering the overall density of the final injection-molded component. Specifically, standard PA66 GF30 exhibits a material density of approximately 1.35 to 1.38 grams per cubic centimeter. In contrast, PA66 CF30 maintains a noticeably lower density of roughly 1.28 to 1.30 grams per cubic centimeter. This density reduction yields immediate component weight savings, which directly benefits dynamic moving assemblies and airborne structures. Furthermore, carbon fibers offer exceptional specific strength and specific modulus, defined as mechanical strength and stiffness divided by material density. The microscopic carbon filaments form an interconnected load-bearing lattice within the PA66 matrix during melt processing, enabling efficient stress distribution. In addition to density benefits, carbon fiber modification markedly improves dimensional stability. Polyamide resins naturally absorb ambient moisture, which typically leads to dimensional expansion and slight reduction in structural stiffness over time. Carbon fibers do not absorb water and exhibit an exceptionally low coefficient of thermal expansion along their longitudinal axis. As a result, PA66 CF30 components demonstrate minimal warpage, precise dimensional retention, and reduced thermal expansion under fluctuating environmental temperatures. Furthermore, carbon fiber imparts natural electrical conductivity and surface static dissipation, whereas glass-filled materials act as electrical insulators. Q2: What Are the Exact Tensile, Flexural, and Thermal Metrics of PA66 CF30—and What Trade-Offs Exist? The integration of 30% carbon fiber dramatically alters the mechanical profile of unmodified Polyamide 66. Neat PA66 resin typically demonstrates a tensile strength of approximately 80 megapascals and a flexural modulus near 2.8 gigapascals. When reinforced with 30% short carbon fiber, the tensile strength escalates to values between 200 and 230 megapascals. More dramatically, the flexural modulus quadruples, reaching impressive values between 18 and 22 gigapascals. This high flexural modulus provides rigid structural resistance against severe bending loads under continuous mechanical stress. Thermal performance also receives a substantial upgrade through carbon fiber modification. Under heavy mechanical loads of 1.8 megapascals, the heat deflection temperature of PA66 CF30 exceeds 250 degrees Celsius. This elevated thermal stability allows structural components to maintain mechanical integrity in hot engine compartments, industrial gearboxes, and high-friction machinery without premature softening. These mechanical gains make the material highly effective in demanding automotive and industrial parts manufacturing workflows. However, objective material selection requires a clear understanding of physical trade-offs. Carbon fiber is inherently stiffer and more brittle than glass fiber. Consequently, while tensile and flexural strengths increase dramatically, the unnotched and notched Izod impact toughness of PA66 CF30 experiences a slight decrease compared to specialized impact-modified or glass-filled grades. Furthermore, carbon fiber raw materials involve higher production costs than standard glass fibers, resulting in elevated material costs per kilogram. Additionally, fiber alignment during injection molding creates anisotropic shrinkage behavior, meaning the material shrinks slightly differently along the flow direction compared to the transverse direction. Engineers must account for these physical characteristics during mold design and cavity sizing. Q3: Where Does PA66 CF30 Excel—and Where Should Alternative Grades Be Selected? Selecting the optimal engineering plastic requires balancing structural performance against cost constraints and environmental conditions. PA66 CF30 excels in applications where weight reduction, structural stiffness, and dimensional accuracy take priority over low initial material cost. In the field of unmanned aerial vehicles and commercial drones, PA66 CF30 provides an ideal material choice for rotor arms, frame connectors, and camera gimbal mounts. The material withstands high vibrational loads while minimizing structural mass, directly extending flight duration and battery efficiency. Similarly, modern robotics and industrial automation rely on PA66 CF30 for articulated joint linkages, robotic gripper arms, and high-speed reciprocating gears. The low inertia of lightweight carbon-reinforced parts allows servo motors to achieve faster response times and higher operational speeds with reduced energy consumption. High-end professional power tools also utilize PA66 CF30 for internal structural chassis and motor housings to reduce overall tool weight and user fatigue. Conversely, applications requiring high impact resistance under extreme shock loading may require alternative material formulations. For example, severe impact environments like heavy construction safety helmets, low-temperature off-road vehicle bumpers, or high-impact athletic protection gear usually benefit more from specialized impact-modified PA66 grades. Furthermore, where electrical insulation is strictly mandatory, non-conductive glass-fiber reinforced PA66 represents the appropriate technical selection. Q4: What Are the Recommended Injection Molding Parameters for Processing PA66 CF30 Compounds? Achieving optimal mechanical performance from PA66 CF30 compounds depends heavily on proper processing techniques during injection molding. Polyamides are hygroscopic materials that absorb atmospheric moisture. Prior to processing, operators must dry PA66 CF30 granules in a dehumidifying desiccant dryer at 80 to 100 degrees Celsius for 4 to 6 hours. Maintaining moisture levels below 0.08% prevents hydrolytic degradation, which can otherwise sever polymer chains and compromise structural strength. The melt processing temperature for PA66 CF30 typically ranges between 285 and 310 degrees Celsius. Maintaining precise barrel temperature profiles ensures proper resin melting without thermally degrading the polymer matrix. Furthermore, mold temperature control plays a vital role in surface quality and mechanical performance. Maintaining a mold temperature between 80 and 120 degrees Celsius promotes uniform polymer crystallization, improves surface appearance, and reduces internal residual stress within the molded part. Engineers must also minimize fiber breakage during plasticization. High screw speeds or excessive back-pressure generate high shear stress, which can crush delicate short carbon fibers and reduce their effective length. Maintaining moderate screw speeds and low back-pressure preserves fiber aspect ratio, maximizing mechanical reinforcement. Because carbon fibers are abrasive, processing facilities should utilize wear-resistant bimetallic barrels and hardened steel molds to ensure long tool life. Q5: How Does BOCHENG Deliver Tailored PA66 CF Compounds and Engineering Support for Global OEMs? To meet diverse industrial requirements, specialized material manufacturers provide tailored compounding solutions that bridge standard resin supply with custom engineering demands. As a dedicated provider of advanced polyamide solutions, BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd) develops high-performance PA66 CF30 compound injection molding grades engineered specifically for structural light-weighting applications. Through precise fiber surface treatment and twin-screw compounding technologies, BOCHENG ensures optimal interfacial bonding between carbon fibers and the PA66 resin matrix. Beyond standard PA66 CF30 formulations, Xiamen Bocheng Plastic Materials Co., Ltd offers customized modification options tailored to specific end-use environments. For applications demanding both extreme rigidity and enhanced toughness, BOCHENG integrates specialized elastomeric impact modifiers into the carbon fiber compound. For high-wear gear applications, the company formulates internal solid lubricants like PTFE or silicone additives to reduce friction coefficients and wear rates. Consistent quality control and technical partnership remain central to industrial material supply. BOCHENG supports global OEMs and molding partners with comprehensive technical assistance, including mold shrinkage estimation, processing parameter optimization, and custom color matching. By combining advanced material performance with responsive engineering support, BOCHENG helps manufacturers successfully replace metal components and achieve lightweight efficiency. For detailed product specifications, technical data sheets, and engineering inquiries, visit the official website at https://www.pa6-pa66.com/.
Read More
The automotive sector is undergoing a profound engineering transformation driven by electrifying drivetrains and downsizing internal combustion engines. Vehicle power density continues to rise rapidly, which concentrates significant thermal energy within compact engine bays and electric drive housings. Consequently, automotive design engineers face mounting pressure to identify structural polymers that maintain long-term mechanical strength under severe heat. Traditional metals once dominated these high-load areas, but their high weight and manufacturing complexity conflict with modern fuel economy and battery range goals. Engineering thermoplastics offer a compelling alternative by combining lightweight properties with the design flexibility of injection molding. However, conventional materials often reach their thermal limits when continuous operating temperatures exceed 150 degrees Celsius. To solve this challenge, material specifiers frequently evaluate specialized High-Temperature Polyamides for Automotive Parts to ensure vehicle safety and durability. Selecting between established aliphatic nylons and advanced semi-aromatic polymers requires a thorough understanding of thermal, chemical, and structural performance metrics. Chemical Architecture: How Aromatic Structure Elevates PPA Above Standard Aliphatic PA66 To evaluate performance differences under thermal stress, engineers must analyze the chemical architecture of both material families. Conventional Polyamide 66 consists of repeating aliphatic hexamethylene diamine and adipic acid molecular chains. This aliphatic structure provides flexible polymer chains that yield excellent mechanical toughness, high tensile strength, and efficient melt processing at moderate temperatures. However, the aliphatic backbone experiences noticeable mobility as temperatures rise toward its glass transition threshold. Unfilled or glass-reinforced PA66 exhibits a glass transition temperature Tg of approximately 60 to 70 degrees Celsius in dry conditions. When operating temperatures surpass this transition point, the polymer matrix undergoes localized softening, which gradually reduces structural stiffness under sustained loads. In contrast, Polyphthalamide, commonly designated as PPA, belongs to the semi-aromatic polyamide family. Material scientists synthesize PPA by replacing portions of aliphatic dicarboxylic acids with aromatic terephthalic or isophthalic acid monomers. The rigid benzene rings embedded within the molecular backbone significantly restrict polymer chain movement under thermal agitation. As a result, PPA exhibits an elevated glass transition temperature Tg ranging from 125 to 135 degrees Celsius. This structural rigidity allows semi-aromatic nylons to preserve mechanical modulus and creep resistance far above the thermal thresholds of standard aliphatic polymers. Furthermore, strong intermolecular hydrogen bonding within the aromatic matrix minimizes thermal degradation during prolonged heat exposure. Head-to-Head Technical Evaluation: HDT, CUT, and Fluid Resistance Metrics Quantitative laboratory testing highlights clear performance disparities between glass-fiber-reinforced PA66 and PPA under thermal and environmental stress. Under a standard mechanical load of 1.8 megapascals, standard PA66 with 30 percent glass fiber reinforcement achieves a heat deflection temperature HDT of approximately 250 degrees Celsius. While this value seems impressive for short-term thermal spikes, continuous exposure to elevated heat tells a different story. The continuous use temperature CUT for glass-reinforced PA66 typically ranges between 130 and 150 degrees Celsius for long-term operational cycles. Beyond these temperatures, thermal oxidation slowly degrades the polymer matrix, leading to brittleness and mechanical fatigue over extended service lifetimes. In comparison, 30 percent glass-reinforced PPA compound demonstrates an HDT reaching between 280 and 290 degrees Celsius under an identical 1.8 megapascal load. More importantly, PPA maintains a continuous use temperature CUT between 170 and 180 degrees Celsius, withstanding intermittent thermal spikes exceeding 220 degrees Celsius without structural collapse. In addition to raw temperature tolerance, chemical and hydrolytic stability play vital roles in under-hood environments. Hot automotive fluids, such as ethylene glycol coolant mixtures, synthetic engine oils, and transmission fluids, aggressively attack aliphatic polyamide chains through hydrolysis. PPA possesses a dense aromatic structure that resists chemical swelling and hydrolytic cleavage. Moreover, PPA absorbs significantly less ambient moisture than PA66, ensuring consistent dimensional tolerances and mechanical stiffness across changing humidity levels. These attributes make PPA a preferred material for critical automotive and industrial parts manufacturing components subject to hot fluid immersion. Application Selection Matrix: Matching Material Capabilities with Cost & Thermal Requirements Although PPA exhibits superior thermal and chemical capabilities, objective engineering decisions must balance performance advantages against manufacturing costs. PPA raw resin carries a higher price tag per kilogram compared to standard PA66 formulations. Additionally, processing PPA requires specialized injection molding machinery capable of maintaining barrel temperatures above 320 degrees Celsius and mold temperatures exceeding 140 degrees Celsius. Consequently, material specifiers must map components accurately into distinct thermal application zones to optimize system costs. PPA compounds serve as the optimal technical choice for high-extreme thermal zones where component failure risks engine performance or electrical safety. Typical applications include turbocharger charge-air duct brackets, electric cooling pump impellers, high-voltage battery busbar housings, and exhaust gas recirculation sensor bodies. In these critical components, PPA replaces heavy die-cast aluminum while surviving continuous exposure to hot gases, aggressive coolants, and intense vibration. Conversely, glass-reinforced PA66 remains the most cost-effective solution for moderate-to-high thermal zones operating reliably below 150 degrees Celsius. Engine beauty covers, intake manifolds, general structural brackets, and wiring conduit clips benefit greatly from PA66 due to its lower raw material cost, broader processing window, and excellent mechanical toughness. Tailored High-Temperature Solutions: How BOCHENG Empowers OEM Component Design Navigating the complex selection process between PPA and PA66 requires reliable compounding expertise and consistent material quality. As a dedicated manufacturer of engineering thermoplastics, BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd) formulates advanced high-temperature polyamide series tailored for demanding automotive and industrial uses. Through precise twin-screw extrusion technology, BOCHENG integrates high-grade glass fibers, flame retardants, and thermal stabilizers into base polymer matrices. The technical portfolio from Xiamen Bocheng Plastic Materials Co., Ltd includes specialized PPA GF30 to GF50 grades designed for extreme under-hood environments, alongside cost-optimized PA66 reinforced compounds for general structural applications. For electric vehicle power systems, BOCHENG provides halogen-free flame-retardant PPA compounds that comply with stringent UL94 V-0 safety standards while maintaining high electrical insulation at elevated temperatures. Furthermore, the technical team at BOCHENG assists Tier-1 automotive suppliers with mold shrinkage calculations, flow analysis, and processing parameter refinement to ensure seamless material substitution. By aligning advanced material chemistry with practical engineering support, BOCHENG enables automotive manufacturers to achieve optimal thermal durability, lightweight performance, and cost efficiency. For comprehensive material datasheets, application engineering support, and product inquiries, visit the official corporate portal at https://www.pa6-pa66.com/.
Read More
As global construction industries pivot toward stringent carbon-neutrality mandates, architectural facade design faces an unprecedented transformation. Regional trade exhibitions like Plast Eurasia serve as vital platforms where material engineers, system fabricators, and building solution providers gather to address these evolving requirements. Within the architectural sector, energy efficiency relies heavily on thermal break systems installed inside aluminum window frames and curtain walls. Meeting these rigorous thermal performance demands requires specialized raw materials capable of enduring high mechanical stress while maintaining dimensional integrity under extreme environmental changes. Recognized as a China Leading PA66 GF25 Thermal Break Strip Material Supplier, the enterprise provides high-performance polyamide granules designed specifically for profile extrusion lines. Industry professionals attending Plast Eurasia continue to discuss how advanced polymer technology can bridge the gap between architectural aesthetics and strict building energy codes across Europe, Eurasia, and the Middle East. Global Decarbonization & Energy Codes: Accelerating Demand for Thermal Barrier Systems Modern building codes across Europe and the Middle East increasingly enforce stricter overall heat transfer coefficients, commonly measured as U-values. High-rise commercial structures and residential complexes demand advanced fenestration systems to minimize thermal conduction. Because aluminum profiles offer exceptional structural strength but high thermal conductivity, window manufacturers must incorporate thermal break strips to separate internal and external aluminum frames. Without effective thermal barriers, buildings experience substantial heat loss during winter and excessive heat gain during summer. Consequently, HVAC systems work harder, raising operational energy consumption and expanding the overall carbon footprint of modern architecture. Regional markets in Eurasia and the Gulf region now require window systems to achieve significantly lower U-values. Therefore, system houses and profile extruders actively seek high-efficiency insulating materials that withstand harsh climate swings while maintaining long-term structural durability. Thermal break strips function as the primary insulating core in aluminum windows, doors, and curtain wall systems. However, choosing the right material involves balancing thermal insulation with mechanical load capacity. Standard polymers often lack the structural rigidity necessary to handle heavy glass loads and severe wind pressures in tall buildings. As a result, polyamide 66 reinforced with 25% short glass fibers has emerged as the definitive material standard across the global construction industry. The Physics of Thermal Breaks: Why PA66 GF25 is the Industry Gold Standard The physical performance of thermal break strips depends on matching the mechanical and thermal properties of the polymer to the surrounding aluminum. Unreinforced plastics expand and contract at rates far higher than aluminum under temperature variations. This discrepancy causes internal stress, delamination, and eventual failure of the window frame assembly over time. Incorporating 25% short glass fiber reinforcement fundamentally alters the physical dynamics of Polyamide 66. This precise glass fiber ratio adjusts the coefficient of thermal expansion of the composite material to approximately 2.3 x 10^-5 / K. This value closely matches the thermal expansion rate of extruded aluminum profiles. Consequently, when temperature fluctuations occur, the aluminum profile and the thermal break strip expand and contract in complete harmony. This mechanical alignment prevents structural separation, frame warping, and seal failure across decades of environmental exposure. Additionally, PA66 GF25 delivers remarkable thermal resistance compared to pure metals. While raw aluminum exhibits a thermal conductivity of roughly 200 W/(m·K), PA66 GF25 reduces thermal conductivity down to approximately 0.30 W/(m·K). This drastic reduction in conductive heat transfer creates an effective thermal barrier within the window assembly. Furthermore, the material offers a high heat deflection temperature exceeding 240 degrees Celsius. This elevated thermal tolerance allows assembled aluminum profiles to undergo downstream electrostatic powder coating and anodizing baking cycles without softening, shrinking, or losing structural shape. Tensile strength values exceeding 80 MPa further ensure that the thermal break strip handles intense wind loads in high-rise curtain wall applications. Extrusion Processing Bottlenecks: Microstructure vs. Macro Precision While PA66 GF25 offers superior physical properties, processing this reinforced compound via continuous profile extrusion introduces complex technical challenges for profile manufacturers. Extrusion operators frequently encounter rheological instabilities, melt fracture, and surface defects during continuous production runs. Because thermal break strips often feature intricate geometric profiles—such as I-shapes, C-shapes, T-shapes, and multi-cavity hollow configurations—maintaining uniform melt flow through the extrusion die demands precise resin chemistry. Uneven glass fiber dispersion within the polymer matrix creates significant processing bottlenecks. Poorly dispersed glass fibers cause localized stress concentration, resulting in brittle strips that snap under mechanical handling. Furthermore, exposed glass fibers on the profile surface create a rough texture. This rough finish hinders smooth insertion into the aluminum profile grooves, leading to assembly delays and profile damage on the factory floor. Moisture management presents another critical processing hurdle during extrusion. Polyamide resin inherently absorbs atmospheric moisture due to its hydrophilic chemical structure. Excess moisture during extrusion triggers hydrolytic degradation, breaking down the polymer chains. This chemical breakdown creates internal micro-voids, reduces mechanical strength, and causes dimensional fluctuations that exceed the tight tolerance limits of plus/minus 0.05 mm required for precision window assemblies. Extruders must therefore utilize compounds designed specifically to maintain melt stability and smooth surface finishes across extended production cycles. BOCHENG’s Engineered PA66 GF25 Solution: Formulated for Precision Extrusion To resolve these processing bottlenecks, advanced compounding technology focuses on molecular structure optimization and surface coupling treatments. BOCHENG (Xiamen Bocheng Plastic Materials Co., Ltd) engineers specialized PA66 GF25 extrusion granules that address the specific needs of thermal break strip manufacturers. By utilizing high-purity polyamide base resins combined with proprietary silane coupling agents, the enterprise ensures uniform glass fiber distribution throughout the polymer matrix. This optimized formulation enhances the interface bonding between the nylon polymer and the glass fibers. As a result, the compound provides superior melt strength and exceptional rheological behavior during high-speed extrusion. The material eliminates surface glass fiber exposure, delivering a smooth matte finish that facilitates seamless insertion into aluminum profile channels. Extrusion facilities using this formulation experience lower die wear, reduced scrap rates, and consistent output speed across complex multi-strand extrusion operations. In addition to mechanical performance, product versatility remains essential for international architectural projects. BOCHENG provides customizable color-matching options, including standard matte black and specialty architectural shades, to match various window design requirements. To verify performance consistency across international markets, the material undergoes comprehensive testing. Manufacturers can inspect the formal compliance and quality certification standards that validate batch-to-batch stability, mechanical strength, and environmental durability. Xiamen Bocheng Plastic Materials Co., Ltd maintains stringent quality control protocols, testing every batch for moisture content, tensile strength, and impact resistance before global dispatch. Strategic Partnership & Technical Co-Development at Plast Eurasia Exhibitions like Plast Eurasia highlight the importance of technical collaboration between raw material compounders and profile extruders. Modern window manufacturing requires more than standardized material supply; it demands comprehensive technical co-development. BOCHENG supports international clients by providing end-to-end engineering assistance, including extrusion die temperature optimization, screw profile advice, and material drying protocols. As building regulations in Europe and Eurasia drive the demand for energy-efficient architecture, sourcing reliable, high-performance thermal break materials becomes a strategic priority. Through continuous innovation in compounding technology, BOCHENG delivers robust polymer solutions that meet international building standards while helping extruders optimize manufacturing efficiency. Extrusions facilities seeking to enhance profile quality and lower production costs can establish direct technical partnerships during industry events or explore specialized material options online. Website: https://www.pa6-pa66.com/.
Read More
From the perspective of polymer melting kinetics, nylon functions as a semi-crystalline engineering thermoplastic whose melting transition involves sharp viscosity shifts and crystallization phenomena. Within a fixed oven residence time and temperature window, particles of varying diameters absorb thermal energy at different rates. Fine particles absorb energy rapidly, melting beyond the phase transition temperature to initiate flow almost instantly; however, premature melting alters local surface tension dynamics. Coarse particles absorb heat with a temporal lag, requiring extended dwell time to erase inter-particle boundaries. If the thermal protocol favors fines, coarse particle cores remain partially unmelted, leaving physical interface boundaries that act as stress concentration sites, severely reducing impact resistance and cross-hatch adhesion. Conversely, if the temperature is elevated to accommodate coarse fractions, early-melting fines suffer thermal-oxidative degradation, causing embrittlement and yellowing. In industrial quality assurance, monitoring D10, D50, D90, and calculating the Span value via laser diffraction sizing represents standard protocol for stable coating engineering. empirical validation indicates that for conventional electrostatic application, maintaining D50 between 35 and 45 microns, D10 above 15 microns, and D90 below 70 microns (targeting a Span between 1.2 and 1.5) delivers optimal electro-dynamic response and film leveling. For fluidized bed applications, maintaining D50 within 80 to 120 microns while strictly limiting fines below 30 microns to under 5% optimizes gas suspension and thermal self-leveling. Tailoring PSD parameters to specific mechanical application protocols eliminates over 90% of raw-material-induced coating defects while dramatically improving transfer efficiency and reclaim stability, ultimately driving down operational manufacturing costs. Mastering particle size distribution shifts nylon coating from empirical trial-and-error to precision processing engineering. Material suppliers and industrial coaters must look beyond standard polymer grade designations or bulk density, integrating PSD metrics into raw material receiving inspections and quality verification frameworks. Establishing a direct analytical database linking grain metrics to shop-floor coating morphology allows processing lines to transition from reactive defect troubleshooting to predictive quality control, ensuring highly durable and consistent nylon barrier layers across demanding industrial environments. FAQ 1. What is your MOQ? For sample orders, we recommend a minimum of 5kg as the MOQ to ensure the validity of the test. For bulk order, we suggest the minimum quantity is 1000kg, the higher the quantity, the lower the shipping cost. 2、About Sample. Samples within 5kg are free of charge, shipping cost is not included. 3、About Quality. We are ISO9001 certified and have perfect testing equipments to ensure that every batch of products are tested and qualified before delivery. 4、About delivery time. Usually samples can be shipped within 3-5 days, and bulk orders can be shipped within 7-10 days. 5、About transaction and payment method. We support TT, LC payment method, EXW, FOB, CIF, CNF trading method.
Read More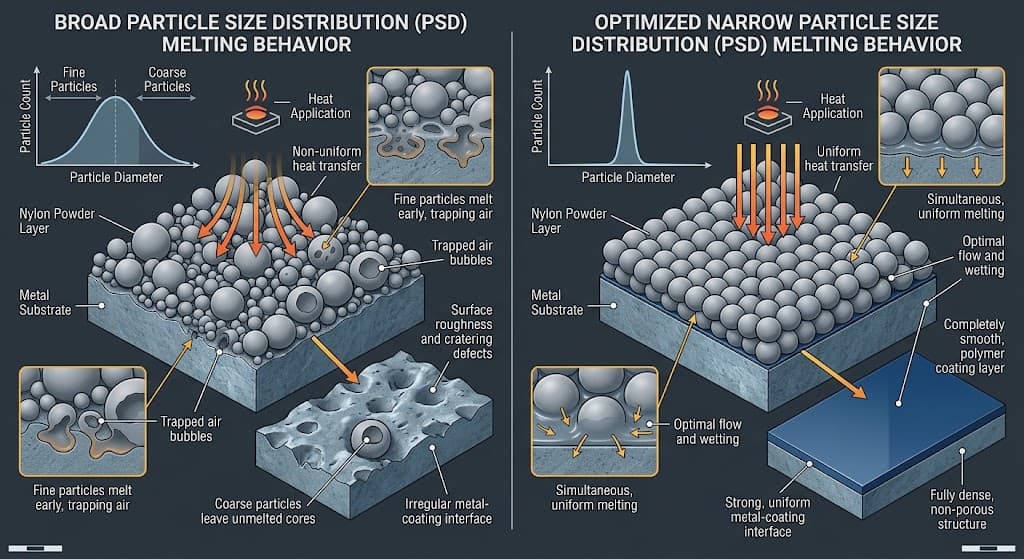
In the practical application of nylon (PA11, PA12) powder electrostatic spraying and fluidized bed dip coating, coating defects such as pinholes, orange peel, uneven thickness, and edge thinning are frequently attributed to baking temperatures or substrate pretreatment. However, deep technical analysis of industrial processing scenarios reveals that many persistent quality fluctuations stem directly from the Particle Size Distribution (PSD) of the feedstock powder. Particle size is far from a simple singular metric; the distinct physical behaviors of coarse and fine particles during fluidization, electrostatic transport, and thermal melting directly dictate the ultimate coating performance in corrosion resistance, mechanical strength, and surface topometry. During electrostatic spraying and fluidized bed processes, powder particles encounter fundamentally different physical forces and heat transfer dynamics. When particles move from the spray gun toward the workpiece under an electric field, aerodynamic drag interacts continuously with electrostatic force. Fine particles (typically defined as those under 20 microns) possess minimal mass and extremely high specific surface area, making them highly susceptible to airflow turbulence and agglomeration. This leads to spitting at the gun nozzle. Once deposited, these agglomerates trap air that struggles to escape during subsequent melt-curing, resulting in microscopic pinholes or cratering defects. Conversely, coarse particles (exceeding 80 or 100 microns) exhibit superior fluidic transfer but lack sufficient electrostatic adhesion, causing premature detachment before entering the oven or sluggish leveling during melting, which manifests as severe orange peel patterns. Fluidized bed coating demands precise suspension control of the powder matrix. An ideal fluidization state relies on uniform gas permeability through particle voids. An excessive ratio of fine powder induces channeling or localized boiling inside the bed. When preheated metal parts are immersed, local regions absorb un-leveled powder agglomerates, causing localized thickness spikes or internal thermal stresses. Conversely, a high concentration of coarse particles causes bed bottom settlement, producing a characteristic gradient where bottom sections are over-coated while top edges are left thin. Consequently, the relative span of the distribution (Span value) provides a much more reliable indicator of line compatibility than the median particle size (D50) alone. Broad distribution powders offer cost advantages, but the melting rate differential between coarse and fine fraction leaves hidden interfacial voids inside the protective layer. FAQ 1. What is your MOQ? For sample orders, we recommend a minimum of 5kg as the MOQ to ensure the validity of the test. For bulk order, we suggest the minimum quantity is 1000kg, the higher the quantity, the lower the shipping cost. 2、About Sample. Samples within 5kg are free of charge, shipping cost is not included. 3、About Quality. We are ISO9001 certified and have perfect testing equipments to ensure that every batch of products are tested and qualified before delivery. 4、About delivery time. Usually samples can be shipped within 3-5 days, and bulk orders can be shipped within 7-10 days. 5、About transaction and payment method. We support TT, LC payment method, EXW, FOB, CIF, CNF trading method.
Read More